During metal machining, temperatures rise rapidly between the cutting tool and the workpiece (the machining zone). With low‑pressure cooling methods, the cutting fluid vaporizes due to high heat before it reaches the machining zone, forming a “vapor film” that blocks further contact between the cutting fluid and the machining zone. Consequently, low‑pressure delivery of cutting fluid delivers almost no cooling or lubrication effect. Excessively high temperatures result in extended cutting paths and produce long, thick chips. This further leads to tool failure, chip tangling around tools, workpiece damage and other issues.
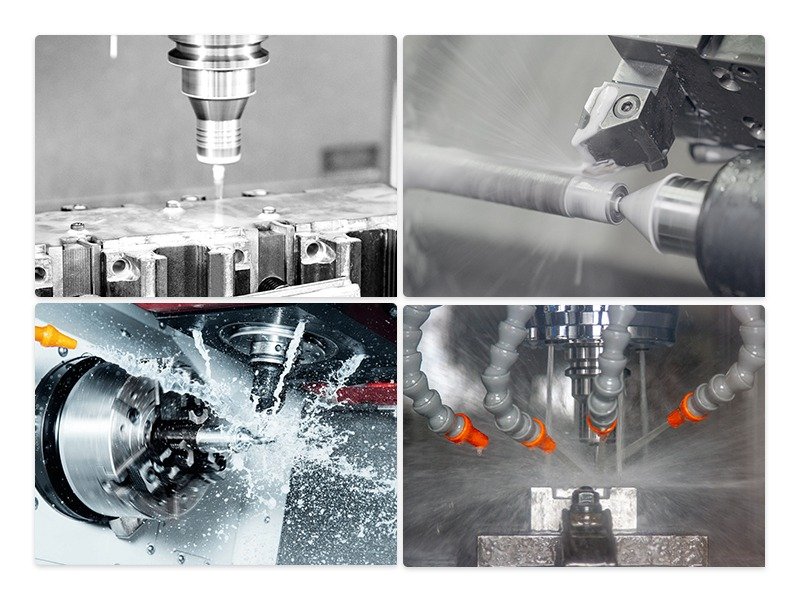
The core solution to the above‑mentioned problems is to deliver cutting fluid to the machining zone to remove heat. Precision‑directed delivery at a high pressure of 7 MPa enables cutting fluid to accurately target the machining zone while penetrating and eliminating the vapor film. When heat is removed in a timely manner, a shorter shear zone forms during machining. Chips curl and break naturally, which reduces tool damage, improves machining efficiency and minimizes workpiece defects. In the long run, this contributes to cost reduction and efficiency improvement.
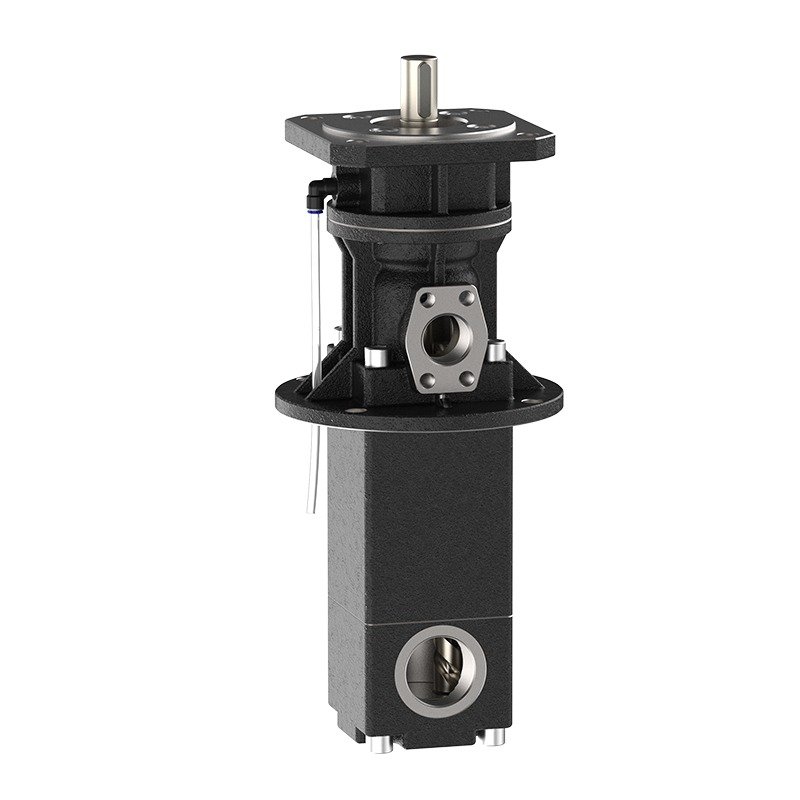
The A3MT‑series high‑pressure coolant pump delivers a maximum outlet pressure of 15 MPa. As a triple‑screw pump, it offers self‑evident advantages. Thanks to the structural characteristics of triple‑screw pumps, it maintains consistent cutting‑fluid output throughout operation. Such stability guarantees the quality of machined parts, which is critical for machine‑tool manufacturers.